NDT for Steel Tubes: Methods and Inspection Requirements
Non-destructive testing (NDT) of steel tubes checks for specified discontinuities without cutting up the tube. For buyers, the important question is not simply whether a supplier offers “NDT,” but which method, inspection coverage, reference standard, and…
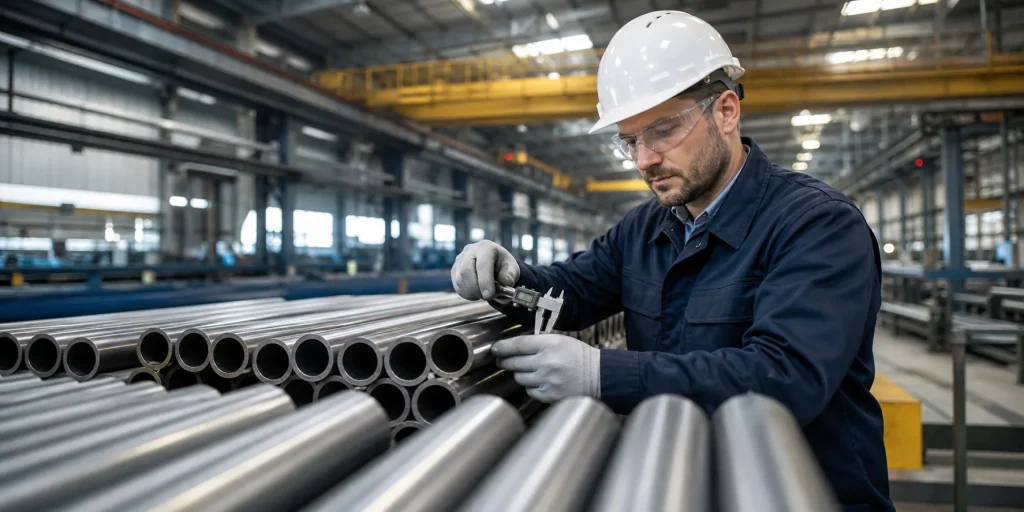
Non-destructive testing (NDT) of steel tubes checks for specified discontinuities without cutting up the tube. For buyers, the important question is not simply whether a supplier offers “NDT,” but which method, inspection coverage, reference standard, and acceptance criteria apply to the ordered material. An inspection result supports a defined requirement; it is not a guarantee that every possible defect has been excluded.
Choose the Method Around the Defect Risk
Begin with the application, tube dimensions, manufacturing route, and likely discontinuity orientation. A hydraulic circuit, machined mechanical component, and welded pressure line can need different inspection plans even when their nominal steel grades are similar. Review the precision tube quality inspection checklist alongside the drawing so dimensional checks and NDT address the same acceptance requirements.
- Ultrasonic testing (UT): Uses sound to examine material below the surface. ASTM E213 describes ultrasonic examination of metal pipe and tubing, including conventional and phased-array techniques. Geometry, beam direction, surface condition, and the validated procedure affect what can be detected.
- Eddy current testing (ET): Uses electromagnetic response to find relevant discontinuities in conductive material. ASTM E309 addresses steel tubular products. Test frequency, coil arrangement, magnetic properties, and line speed influence sensitivity; ET should not be described as a universal deep-wall inspection.
- Magnetic particle testing (MT): Can reveal surface and near-surface discontinuities in ferromagnetic material. It is not suitable for every alloy, and magnetization direction matters.
- Liquid penetrant testing (PT): Reveals discontinuities open to a prepared, nonporous surface. It does not examine the tube wall internally.
- Radiographic testing (RT): Uses X-rays or gamma rays to form an image of internal structure. Its suitability depends on the part and examination objective, and it requires appropriate radiation controls.
The American Society for Nondestructive Testing’s method overview explains these differences. No single method replaces every other inspection or establishes fitness for a particular pressure or fatigue duty.
What Automated and Phased-Array Inspection Changes
Automation can make a defined scan more repeatable and connect indications to a tube or production lot. Phased-array ultrasonic testing uses multiple transducer elements to control the sound beam electronically. These are useful inspection tools, but the equipment label alone does not establish coverage or acceptance.
For example, ISO 10893-10 covers automated full-peripheral ultrasonic testing for longitudinal and/or transverse imperfections in specified seamless and welded steel tubes, excluding submerged-arc-welded tubes. A buyer should identify the applicable part, edition, amendments, acceptance level, and product-standard requirements rather than requesting “ISO testing” without further detail.
Ask how the inspection treats tube ends, changes in section, and the smallest ordered dimensions. If a scanning arrangement leaves an untested region, the order should state how that region is controlled, examined separately, or removed. Digital records are useful only when the procedure and physical tube identity remain connected.
Define Acceptance Before Production
A test-method standard explains an examination process; it does not necessarily supply the acceptance criteria for the finished product. ASTM E309, for example, explicitly leaves acceptance criteria to the using parties. Avoid an order that says only “UT passed” or “100% ET” without defining what those statements mean.
A practical inspection request should include:
- The tube standard, grade, delivery condition, outside diameter, and wall thickness.
- The NDT method, procedure reference, applicable standard edition, and personnel qualification requirements.
- The inspection extent and directions, including how end zones or other coverage limitations are handled.
- The agreed reference discontinuities, sensitivity settings, and acceptance or rejection rules.
- The reporting, traceability, and any purchaser witness or third-party inspection requirements.
Keep pressure or leak testing separate in the specification unless the governing product standard expressly permits a defined alternative. Demonstrating sensitivity to a reference discontinuity is not the same claim as demonstrating leak-tightness under a specified pressure test.
Read the Report as Part of the Lot Record
At release, reconcile the inspection report with the heat number, production lot, tube marking, and purchase order. Check that the recorded dimensions and delivery condition describe the supplied material, not a previous qualification sample. If the record states only a method abbreviation and “acceptable,” request the procedure, acceptance reference, and coverage information needed to interpret it.
Our guide to steel tube material traceability explains why those connections matter. NDT does not replace chemical analysis, mechanical testing, dimensional inspection, or the required inspection certificate; each answers a different procurement question.
Specify a Testable Requirement, Not a Marketing Claim
Before requesting a quotation from Tenjan, prepare the drawing, end-use requirements, material specification, and required inspection documents. Ask which NDT methods and coverage can be offered for that particular tube and obtain written confirmation before ordering. The supplier evaluation guide can help structure that discussion. Confirmed, application-specific requirements are more useful than an unsupported claim that a process detects every defect.